Blog Details
Read the latest news, technical articles,
and industry updates from our experts.
Spiral Conveyor for Manufacturing Plants
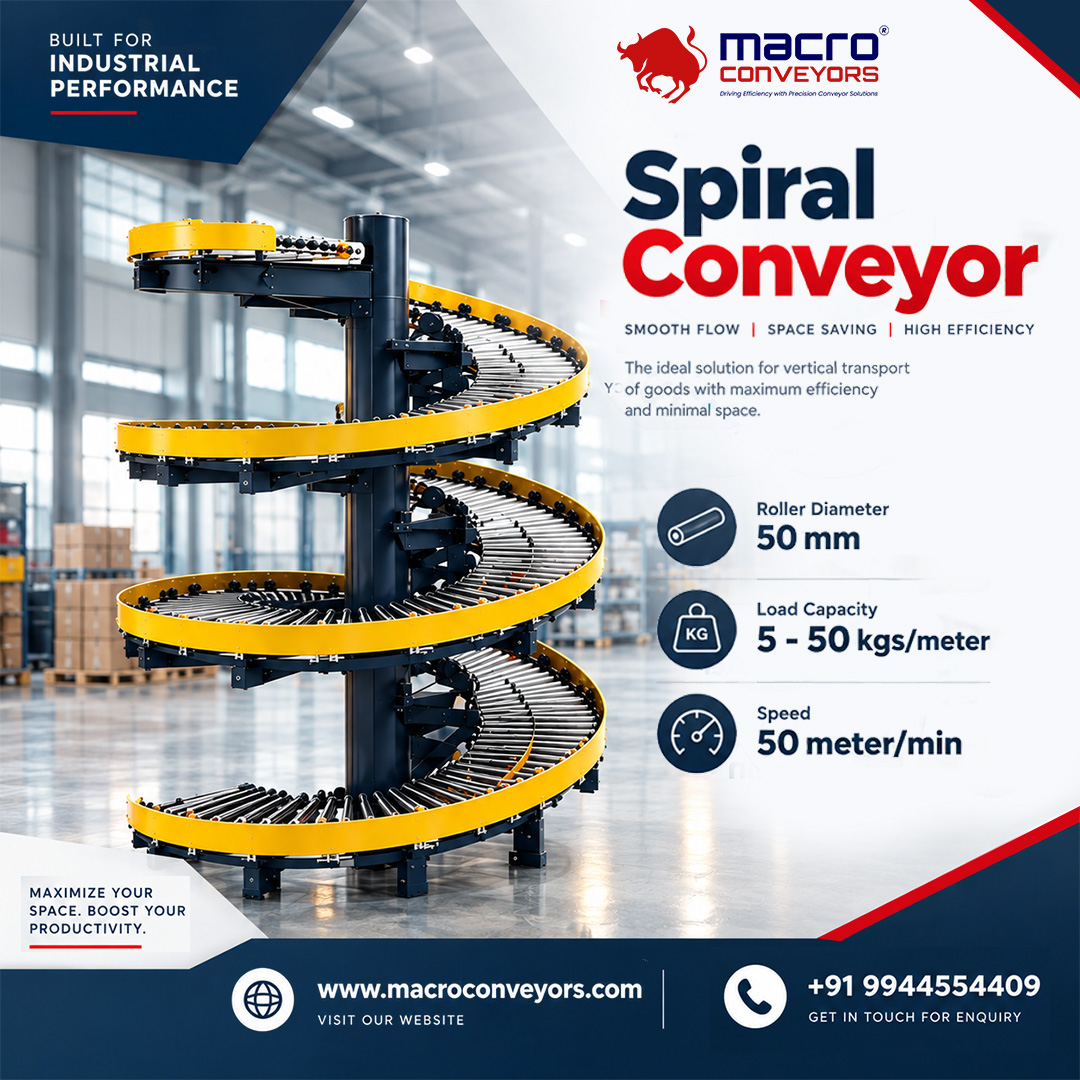
Modern manufacturing industries require efficient material handling systems to maintain smooth production flow, reduce manual handling, and improve operational productivity. A Spiral Conveyor for Manufacturing Plants is a practical material handling solution designed to move products vertically between different production levels while using minimal floor space.
A spiral conveyor is a material handling system that transports products continuously along a spiral-shaped path. Unlike conventional inclined conveyors that require a long horizontal footprint, a spiral conveyor moves products upward or downward around a compact vertical structure.
This configuration helps manufacturing facilities make better use of available floor space while maintaining a continuous product flow. Spiral conveyors can be designed for compatible products, packaging types, load requirements, and production speeds.
They are commonly considered for facilities where products need to move between different elevations without interrupting the overall manufacturing process.
Macro Conveyors provides material handling conveyor solutions for industrial applications. Spiral conveyors can be incorporated into manufacturing and packaging lines to support product movement between floors, processing stages, and conveyor levels, depending on the layout and operational requirements.
Importance of Spiral Conveyors in Manufacturing Industries
Material movement is an essential part of manufacturing operations. Products may need to travel from production machines to inspection stations, packaging lines, storage areas, or dispatch sections. Inefficient movement can create bottlenecks, increase manual handling, and affect production flow.
A spiral conveyor provides a compact way to connect different levels within a facility. By integrating it with existing conveyor systems, manufacturers can organize material movement more efficiently and improve the use of available production space.
For industries with continuous production requirements, selecting a suitable conveyor system can help support a more organized material handling process.
Applications of Spiral Conveyors in Manufacturing Industries
Common Applications
- Packaging Industries
- Food and Beverage Manufacturing
- Pharmaceutical and Healthcare Products
- Automotive and Engineering Industries
- Warehousing and Distribution
- Consumer Goods Manufacturing
Key Benefits of Spiral Conveyors
- Space-Saving Design
- Continuous Product Movement
- Improved Production Flow
- Reduced Manual Handling
- Flexible Conveyor Integration
- Better Use of Vertical Space
The conveyor’s operation depends on its drive arrangement, conveying surface, product characteristics, required throughput, and system controls. Properly designed infeed and discharge sections help maintain stable product movement and integration with the rest of the production line.
Why Choose Macro Conveyors?
Macro Conveyors focuses on material handling conveyor solutions for industrial and manufacturing applications. When evaluating a spiral conveyor, manufacturers should consider their available floor space, transfer height, product specifications, production rate, and connection with existing equipment.
A suitable conveyor configuration can help streamline vertical product movement and support an organized manufacturing workflow. Equipment selection should be based on the actual operating conditions and the requirements of the production facility.
Businesses looking for a Spiral Conveyor for Manufacturing Plants can assess their material handling needs with Macro Conveyors to determine an appropriate conveyor arrangement for their application.
A Spiral Conveyor for Manufacturing Plants offers a space-conscious approach to transferring compatible products between different production levels. Its vertical conveying path can support applications in packaging, food and beverage manufacturing, pharmaceutical packaging, automotive production, consumer goods, and warehousing.
By considering product dimensions, throughput, transfer height, available space, safety, and conveyor integration, manufacturers can identify a system that meets their operational requirements.
Macro Conveyors provides material handling conveyor solutions for industrial applications, helping businesses evaluate conveyor configurations suited to their production layouts and product movement needs.
Keywords
- Spiral Conveyor for Manufacturing Plants
- Spiral Conveyor for Packaging Industries
- Spiral Conveyor System for Production Lines